Skip to content
Apparel Testing & Laboratory Coordination for Fashion Brands
Testing support built into dress development, sample approval, bulk production and controlled delivery.
Duolan coordinates client-required apparel testing as part of a structured womenswear manufacturing program. Formal tests and official reports are completed by qualified or brand-appointed laboratories; our production teams manage the materials, samples, documents, schedules and corrective actions needed to keep testing connected to real bulk execution.
- 16 owned womenswear factories supported by 20+ long-term satellite factories across the group network.
- 300 garment sewing lines, including 50+ quick-response and flexible lines for multi-style programs.
- 15,000-35,000 sample development pieces or style iterations supported each month across the group.
- Testing coordination aligned with client protocols, approved laboratory lists and project deadlines.
- Fabric, trim and garment results transferred into PP approval, BOM control, inline QC and reorder records.
- SMETA 2-Pillar audit record with support for client-specific quality, social and testing requirements.
Testing Coordination Built for Established Fashion Teams
Brand QA Teams
Buying and Sourcing
Product Development Teams
Production Operations
Production teams require a controlled handover from approved sample to bulk. Material codes, approved lots, test reports, PP comments, inspection points and packaging instructions must agree. Our group structure supports centralized documentation and factory-level execution so an approved result is not separated from the material and process used in production.
Testing Risks Become Expensive When Found Too Late
Wrong Test Scope
Late Sample Submission
Unapproved Laboratory
Untraceable Test Sample
Fail Without Closure
Report Production Gap
Passing data must reach the production floor. Material locking, PP sample notes, pre-production meetings, first-piece checks and inline inspection criteria are updated so the tested condition is reproduced in bulk rather than remaining in a document folder.
Clear Responsibilities Across Testing and Production
Defined ownership protects report credibility and prevents a manufacturing supplier from being presented as an accredited testing body.
| Workstream | Duolan | Third-Party Laboratory | Brand Team |
|---|---|---|---|
| Project requirements | Organizes product, material, timeline and production information. | Confirms sample and method requirements for the requested work. | Provides market, protocol, RSL, approved lab and pass criteria. |
| Test scope | Flags product and material risks and coordinates missing inputs. | Confirms methods, conditions, sample quantity and laboratory capability. | Approves the final scope and any brand-specific deviation. |
| Sample submission | Prepares traceable fabric, trim or garment samples and TRF information. | Receives and logs samples, then performs accepted methods. | Confirms nominated laboratory and required report route. |
| Formal report | Tracks status, verifies project references and distributes records. | Issues the official laboratory report within its accreditation scope. | Reviews acceptance, waiver or escalation requirements. |
| Failed result | Coordinates root-cause review, correction, replacement sample and retest. | Provides measured results and available technical clarification. | Approves corrective action, concession or material replacement. |
| Bulk controls | Updates BOM, PP notes, production instructions and QC checkpoints. | Normally does not control garment production. | Confirms release conditions and report retention rules. |
Apparel Tests Coordinated Around Product and Market Risks
Dimensional Performance

Color Performance

Fabric Durability
Pilling, abrasion, tensile, tear, seam-related and snagging risks influence how a fabric performs during fitting, wear and repeated care. Test selection focuses on the fabric structure and garment stress points rather than an undifferentiated checklist.

Stretch and Recovery

Chemical and RSL

Composition and Labels
Testing Priorities for High-Risk Fashion Dress Categories
Fashion dresses combine visual impact with demanding materials and structures. Testing priorities should follow the failure modes most likely to affect fit, appearance and bulk repeatability.
| Dress Direction | Priority Risks | Coordinated Testing Focus | Bulk Control Response |
|---|---|---|---|
| Satin dresses | Shrinkage, snagging, shade variation, seam marking and wash appearance. | Dimensional stability, colorfastness, snagging or protocol-specific appearance tests. | Lock fabric lot and cutting direction; control needle, pressing, handling and protective packing. |
| Bodycon and fitted dresses | Recovery loss, transparency, growth and measurement drift. | Stretch and recovery, dimensional stability, weight and opacity review where required. | Lock stretch direction, pattern reduction, lining, seam construction and size tolerances. |
| Mesh and lace dresses | Tearing, snagging, transparency, seam distortion and lining mismatch. | Strength, dimensional, colorfastness and client-required safety or chemical tests. | Control lining coverage, seam allowance, reinforcement, tension and packaging. |
| Sequin and embellished dresses | Attachment loss, abrasion, sharp edges, color transfer and care damage. | Attachment, durability, color or restricted-substance work required by the protocol. | Approve trim lot, attachment method, back-side comfort, inspection level and packing protection. |
| White and pale dresses | Opacity, lining show-through, yellowing and color contamination. | Opacity review, dimensional stability, transfer or care-related tests when specified. | Control lining shade, storage, clean production handling and individual protection. |
| Printed or contrast styles | Bleeding, crocking, print cracking, migration and panel staining. | Washing, rubbing, perspiration, adhesion or brand-specified print tests. | Approve print batch, panel combination, care method and separation during packing. |
Aligning Test Methods with Markets and Brand Protocols
Market and Product Requirements
- Product definition: adult fashion dress, youth product, fitted knit dress, embellished style or another declared category.
- Destination: selling markets, retailer channels and any market-specific product claim.
- Material system: shell, lining, interlining, elastic, print, coating, metal, beads, sequins and adhesives.
- Care route: wash, dry-clean, hand-wash, steam or other approved instruction affecting test conditions.
Client Testing Protocol
Established brands often provide a testing manual, restricted substances list, approved laboratory list, report naming convention, submission form and pass/fail criteria. Those documents take priority over a factory-created generic package. Our coordination begins by identifying missing inputs and potential conflicts: a protocol may request a method not offered at the nominated location, a colorway may require separate submission, or a deadline may not allow standard turnaround.
Questions are raised before dispatch so the brand can approve the route rather than discovering a mismatch after the report is issued.
- Accepted inputs: brand testing manuals, RSL or MRSL files, quality manuals, vendor compliance documents and approved lab lists.
- Controlled references: style number, purchase program, color code, fabric supplier, lot or batch and report deadline.
- Approval points: test scope, laboratory location, sample quantity, method, pass level and report distribution.
Laboratory Scope and Acceptance
A recognized company name does not automatically mean every laboratory location is approved for every method. Before submission, the exact facility, test method, accreditation scope, sample requirement, turnaround and report format should be confirmed. Duolan can coordinate with a brand-appointed laboratory or help collect options for brand approval when no laboratory has been nominated. We do not represent an internal factory check as an accredited laboratory result. Internal inspections support material screening and production control; official test reports remain the responsibility of the third-party laboratory.
- Verify the exact laboratory address and responsible account contact.
- Confirm the method appears within the laboratory capability or approved scope required by the brand.
- Confirm standard and expedited turnaround before linking the report to production release.
- Confirm whether reports must be uploaded to a brand portal, sent to a nominated team or retained by the supplier.

Testing Timing Across Development and Bulk Production

Material Development Stage
- Typical planning window: before final fabric booking and PP sample preparation.
- Main output: material risk decision and follow-up actions.

Sample and Fit Stage
Garment construction can create risks not visible in a loose swatch. Lining, interlining, boning, elastic, prints, trims, contrast panels and seam stress may change the required submission.
Fit and revised samples also reveal where dimensional change, stretch loss or seam performance would affect the intended silhouette.
- Typical planning window: first sample through revised fit approval.
- Main output: confirmed garment-level risks and test sample plan.

PP and Bulk Stage
- Typical planning window: before bulk cutting or the brand-defined release gate.
- Main output: report status tied to PP and production authorization.

Reorder and Change Stage
A reorder is not automatically identical. New dye lots, colors, suppliers, prints, coatings, trims, care instructions or selling markets can change the risk profile. Existing reports are reviewed against the new order rather than copied without checking scope, validity and material correspondence.
- Typical planning window: before material confirmation for the repeat order.
- Main output: retest, extension, document reuse or brand approval decision.
Our Apparel Laboratory Coordination Workflow
Eight controlled steps keep the testing route connected to materials, samples, production and final report closure.
Requirement Intake
Risk Scope Review
Laboratory Confirmation
Sample Planning
TRF and Submission
Status Tracking
Report Review
Closure and Update
Information Needed Before Testing Coordination Begins
Product Information
- Style and color list
- Fabric, lining and trim details
- Tech pack or construction notes
- Reference sample or approved swatch
Compliance Information
Provide target markets, brand testing protocol, restricted substances list, quality manual, approved laboratory list, report naming requirements and any retailer-specific conditions. Where the protocol is incomplete, Duolan records open questions instead of choosing legal or brand requirements without authorization.
- Testing manual
- RSL or MRSL
- Approved lab list
- Pass criteria and report route
Timeline Information
Provide the current sample stage, PP target, fabric booking date, bulk start, planned shipment and required report date. Standard laboratory turnaround can vary by method and sample condition, while retesting creates additional time. Testing should therefore be planned as a production gate rather than an afterthought.
- Sample status
- Required report date
- PP and bulk dates
- Shipment or launch deadline
Fabric Testing Before Dress Production Risks Become Bulk Issues

Dimensional Stability and Pattern Allowance
- Pattern response: length, width, seam matching and tolerance may require adjustment before final PP approval.
- Production response: fabric relaxation, spreading, cutting and pressing conditions are recorded for the applicable material.
- Quality response: selected dimensions receive focused first-piece and inline checks when shrinkage could alter fit.

Stretch Recovery and Fitted Silhouettes
- Material response: compare extension and recovery by direction, color and lot when the protocol requires it.
- Sample response: verify opacity, compression, comfort and seam behavior on the fitted garment.
- Bulk response: control lay direction, cut-part labeling, elastic application, stitch balance and measurement drift.

Colorfastness and Multi-Material Dresses
Dark shells, pale linings, contrast panels, printed surfaces and decorative trims can create color transfer risks even when each material appears acceptable alone. Washing, rubbing, perspiration or water exposure may affect adjacent components differently. Test planning therefore follows the complete color and material combination. Production controls include approved shade references, supplier lot records, clean handling, component segregation and packing protection.
Where a failed color result leads to an improved dyeing or finishing process, the replacement material and retest sample are linked to the revised bulk lot so the correction remains traceable.
- Development check: assess high-risk dark/light combinations before the collection depends on the color direction.
- Submission check: identify shell, lining, trim and print color codes clearly on the TRF and sample.
- Production check: prevent mixing of unapproved lots and monitor shade consistency across panels and units.

Weight, Opacity and Surface Durability
Fabric weight, opacity, pilling, abrasion and snagging influence both visual quality and commercial wear. A pale jersey may pass composition and color tests yet remain too transparent under stretch; a satin may maintain strength but snag during sewing and packing; a brushed knit may develop surface change in high-friction areas. Duolan uses available test results with sample observation rather than treating one measurement as a complete quality verdict. Material selection, lining coverage, seam placement, needle choice, pressing and protective packing are adjusted around the actual dress construction.
- Across the group network, approximately 1,100-2,000 units support fabric inspection, spreading and cutting functions, including inspection machines, weight checking, light boxes, automatic spreading and computerized cutting equipment.
- Internal screening supports production decisions but does not replace official laboratory testing required by the brand.
- Visible evidence should include test swatches, wash comparisons, light-box shade review, fabric codes and redacted report references.
Testing Considerations for Trims and Embellished Dresses

Sequins, Beads and Stone Attachment
- Development evidence: decoration board, stitch trial, reverse-side close-up and wear-contact review.
- Production evidence: approved trim lot, machine setting, operator standard, inline pull checks and defect classification.
- Group capacity includes approximately 150-300 embroidery units, covering single-head, multi-head, sequin and related embroidery equipment across the manufacturing network.

Metal Trims and Decorative Components
Buckles, hooks, chains, eyelets, sliders, stones and other decorative components can affect safety, comfort, corrosion, finish durability and restricted-substance compliance. The brand protocol determines whether nickel release, heavy metals, sharp-point, coating or other tests apply. Duolan records component supplier, finish, color, lot and placement so the submitted trim corresponds with the approved garment. Construction review also considers reinforcement, skin contact, pull direction and the possibility of damage during finishing or packing. Replacement components are not introduced into bulk without updating the approved reference and any testing requirement.
- Required inputs: trim specification, plating or finish, supplier reference, skin-contact position and brand RSL.
- Control points: incoming inspection, appearance standard, attachment method, pull direction and replacement authorization.
- Report linkage: component code and applicable style/color must be visible in the document trail.

Prints, Coatings and Adhesive Processes
- Before testing: confirm fabric lot, print recipe, curing route and intended care instruction.
- Before bulk: approve strike-off, placement, hand feel, stretch behavior and color relationship.
- During production: monitor curing, alignment, contamination, cracking and lot consistency.

Elastic, Zippers and Fasteners
Elastic, concealed zippers, hooks, snaps and fasteners influence fit, dressing function and long-term appearance. Fitted dresses can fail commercially when elastic grows, zipper tape ripples, sliders catch, hooks distort or reinforcement is insufficient. Protocol-driven tests may cover extension, fatigue, pull, operation or restricted substances. Duolan combines component information with construction trials, sample fitting and production checks. The approved component supplier and code are locked in the BOM, while first-piece and inline checks focus on insertion length, tension, alignment, reinforcement and repeated operation.
- Sample review: operate closures repeatedly and inspect distortion, puckering and stress concentration.
- Production review: verify component lot, insertion method, reinforcement and finished opening length.
- Change control: substitutions require approval and a new testing assessment where the protocol demands it.
Matching Material Documents to Actual Production Materials
Requirement Review
Brand manuals are checked for required document type, issuing body, validity, report language, supplier name and material coverage. A general certificate is not treated as proof for every fabric, color, trim or order. Open questions are returned for brand confirmation before labels or claims are finalized.
- Target claim or requirement
- Accepted issuing body
- Validity and scope
- Required report or certificate format
Supplier File Collection
- Supplier and mill identity
- Material code and construction
- Color or lot coverage
- Issue date and validity
Material Style Matching
- Shell, lining and interlining
- Elastic, zipper and metal trim
- Print, coating and decoration
- Style and color references
Client Review Package
A controlled file package can include submission records, official reports, supplier documents, material references, corrective action and retest evidence. File names and status labels should allow the brand team to see what is approved, pending, failed, replaced or no longer applicable without searching across disconnected email chains.
- Approved and pending status
- Report number and date
- Applicable style/color
- Reorder or change notes
How Failed Test Results Are Investigated and Closed
Confirm the Failure
Trace the Sample
Review Root Cause
Define Corrective Action
Prepare Retest Sample
Update Production Controls
After acceptance, BOM, PP notes, incoming inspection, pre-production meeting, first-piece criteria and inline QC are updated. Reorder files retain the failure and correction history to prevent recurrence.
Turning Laboratory Results into Bulk Production Controls
Material Locking and BOM Control
Approved results are linked to the exact shell, lining, interlining, elastic, zipper, trim, print or coating reference used for the order. Supplier, material code, color, lot or applicable batch, composition and relevant report number are recorded in the project file. Substitution is controlled because a similar-looking material can perform differently in shrinkage, recovery, color transfer or chemical scope. Incoming inspection verifies identity and visible consistency before cutting.
For multi-factory allocation, the same approved references and change-control rules are distributed to each production location.
- Material release requires a confirmed relationship between the report and the booked production material.
- Alternative materials remain pending until technical and compliance review is complete.
- Color and lot changes are assessed against the brand retest or extension policy.
PP Sample and Pre-Production Alignment
- Confirm the PP sample uses the approved materials and component codes.
- Record test-related risks in the pre-production meeting and operation standards.
- Hold production release when a required report remains failed, missing or mismatched, subject to brand authorization.
First-Piece and Inline QC Updates
- Risk-based checkpoints are assigned by style instead of applying one identical checklist to every dress.
- Findings are recorded with style, size, color, line and corrective action information.
- Repeated defects trigger process review, not only piece-by-piece repair.
Reorder Records and Change Management
Repeat orders benefit from archived patterns, BOMs, approved samples, test reports, failure records and corrective actions, but reuse is not automatic. New colors, fabric lots, mills, trims, prints, finishes, factories, markets or care instructions can alter the testing requirement. Before a reorder is released, the current material and production plan are compared with the archived approval. The brand protocol determines whether an existing report remains valid, whether an extension can be accepted or whether a new test is required. Clear records shorten review without weakening control.
- Archive package: applicable report, material reference, PP approval, QC notes and change history.
- Reorder review: identify every difference from the previously approved order.
- Brand decision: reuse, extension, supplementary test or full retest according to the approved policy.
Evidence Behind Our Testing Coordination Capability
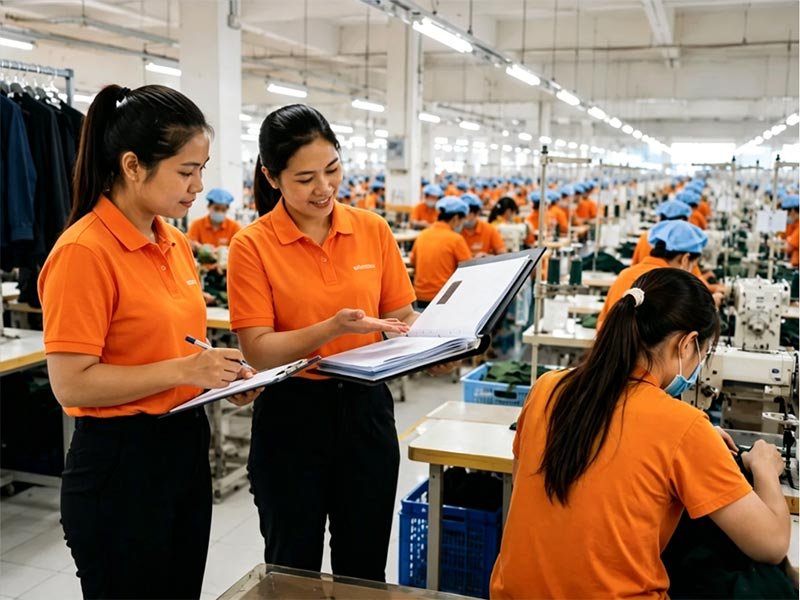
Audited Manufacturing Base

Multi-Factory Control

Development Capacity

Production Infrastructure
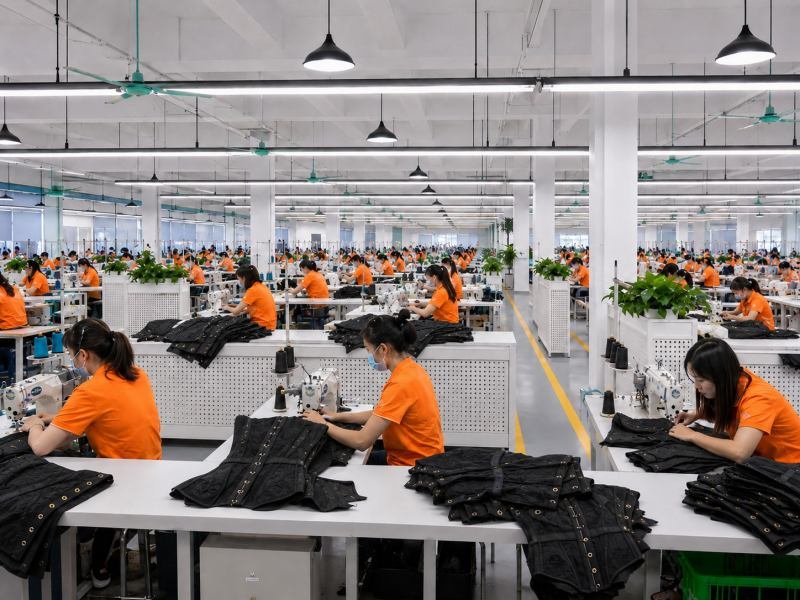
Inspection Resources

Special Process Network
Printing, embroidery, washing and finishing resources are coordinated through mature internal and partner facilities. Around 150-400 printing units and 150-300 embroidery units support fashion dress programs requiring controlled decorative processes.
Testing Coordination from Material Risk to Bulk Approval
Representative 18-Style Occasion Dress Program
- Program size: 18 styles, 37 color-style combinations and 48,600 total garments.
- Material scope: 14 shell fabrics, 7 linings, 9 trim or decoration groups and 5 print/finish routes.
- Submission scope: 46 fabric, trim and garment test submissions, including color-specific or component-specific sets required by the protocol.
- Development route: first sample, fit revision, PP approval, controlled testing gates and multi-factory bulk allocation.
Risk Findings and Corrective Actions
- Material corrections: 2 dyeing or finishing adjustments, 1 jersey lot replacement and 2 mesh process revisions.
- Construction corrections: 3 trim attachment updates involving stitch path, backing or reinforcement.
- Process correction: 1 print curing update followed by a controlled replacement sample.
- Document control: each correction was linked to the revised material code, applicable style/color and retest record.
Production Release and Delivery Control
Approved results were transferred into BOM revisions, PP sample records, pre-production meeting notes and style-specific QC checkpoints. Satin styles received added shade, handling and pressing controls; bodycon styles received stretch-direction, measurement and recovery-sensitive checks; embellished styles received attachment and back-side comfort inspection; mesh styles received lining coverage and seam-tension control. Production was distributed across owned factories according to process complexity, while common files and escalation rules remained centralized. The program was released in planned production waves rather than waiting for every style to reach the same stage.
- Testing and correction window: 19 calendar days from first laboratory receipt to closure of the final retest set.
- Bulk structure: 3 controlled production waves aligned with material readiness and approved report status.
- Quality handover: 18 style control sheets updated with test-linked material and process checkpoints.
- Final outcome: all required report routes closed before the related production release gate; no blanket claim of zero defects or universal test coverage is made.

Apparel Testing Frequently Asked Questions
Share Your Testing Protocol and Production Plan
Send your dress program information before fabric booking, PP approval or bulk release. Duolan will review the available product, material, testing and timeline inputs, identify missing coordination items, and prepare a production-focused discussion for laboratory submission and follow-up. The review does not replace legal advice, brand compliance approval or an accredited laboratory report. It helps connect those requirements with sample development, material control, corrective action and bulk manufacturing.
- Style list, tech packs and product categories
- Target markets and selling channels
- Shell, lining, trim, print and decoration details
- Testing protocol, RSL or quality manual
- Approved laboratory and report distribution route
- Required report date, PP target, bulk start and shipment plan
- Previous failed reports or unresolved material concerns
- Expected program range, including styles, colors and order quantities